Overview: What RAMI 4.0 Represents
RAMI 4.0, the Reference Architectural Model for Industry 4.0, was initially standardized as DIN SPEC 91345:2016 and later aligned with IEC PAS 63088. It emerged from German industry efforts to provide a structured way of describing the components, relationships, and data flows that characterize modern manufacturing systems. The model is a conceptual, three-dimensional reference architecture, not a concrete system blueprint or implementation method.
The purpose of RAMI 4.0 is to serve as a shared mental model and common language for describing Industry 4.0 systems, physical assets, and data flows across disciplines. Engineers, software vendors, automation specialists, and standards bodies can use the same coordinate system to discuss where a given technology, standard, or function belongs within a broader manufacturing context. This is particularly valuable in environments where information technology and operational technology must converge.
The model helps position technologies such as digital twin implementations, OPC UA communication protocols, and smart sensors within a consistent architectural frame. However, RAMI 4.0 remains technology-agnostic. It does not mandate specific products, platforms, or integration patterns. This article is written from Connect981’s perspective as an aerospace and MRO operations platform, using RAMI 4.0 purely as a reference explanation without prescribing adoption or implementation steps.
Industry 4.0 Context and Motivation
The term Industry 4.0 situates current manufacturing transformation within a historical sequence. The First Industrial Revolution brought mechanization through water and steam power. The Second introduced mass production and electrical engineering. The Third applied electronics and information technology to automate industrial processes. The fourth industrial revolution, emerging around 2011 onward, centers on cyber physical systems, the Industrial Internet of Things, and data-driven automation.
Germany’s “Plattform Industrie 4.0” served as a central driver for this movement. The initiative brought together representatives from mechanical engineering, electrical engineering, and information and communication technology sectors to define a coherent vision for networked production. The goal was not merely to introduce advanced technologies but to enable manufacturing companies to operate with greater efficiency through connected, intelligent systems.
The complexity of heterogeneous technologies, standards, and domains made a reference architecture necessary. Enterprise IT systems, shopfloor control systems, field devices, and products each brought their own conventions and protocols. Prior models like ISA-95 and IEC 62264 addressed automated interfaces between enterprise and control systems. Life cycle management standards such as IEC 62890 covered industrial system lifecycles. However, neither offered a unified view of Industry 4.0 that could span all these concerns.
For sectors like aerospace manufacturing and MRO, clear reference models help reason about traceability, digital documentation, and multi-tier supply chain integration. Even if RAMI 4.0 itself does not dictate concrete automation solutions, it provides a vocabulary for discussing where different systems and functions belong in a broader architecture.
Origins and Standardization of RAMI 4.0
The development of RAMI 4.0 began around 2013-2015 through the collaborative efforts of German “Plattform Industrie 4.0” working groups, together with VDI (Association of German Engineers) and ZVEI (the German Electrical and Electronic Manufacturers Association). These organizations recognized that without a common framework, Industry 4.0 efforts would fragment into incompatible implementations.
Key milestones in the standardization process include:
Milestone
Year
Significance
Initial RAMI 4.0 concept publication
2015
ZVEI status report establishing the three-dimensional model
DIN SPEC 91345
2016
German national standard formalizing RAMI 4.0
IEC PAS 63088
2017
International alignment through IEC Publicly Available Specification
The purpose of RAMI 4.0 from the outset was to harmonize existing and emerging standards, not to replace them. The model gives stakeholders a shared three-dimensional map for positioning international standards and use cases. Government-backed initiatives in Germany aimed to avoid fragmentation by promoting RAMI 4.0 as a common reference, especially for machine builders, automation vendors, and software providers.
The industrial internet reference architecture (IIRA), developed by the Industrial Internet Consortium, emerged in parallel for broader IIoT contexts. RAMI 4.0 focused specifically on manufacturing and industrial production, reflecting its German manufacturing origins and strong anchoring in European standardization for various industries.
RAMI 4.0 as a Three-Dimensional Reference Architecture Model
RAMI 4.0 uses a three dimensional coordinate system to map any Industry 4.0 concept, component, or function. The three axes are:
- Layers (vertical axis): Representing IT representation of assets
- Life Cycle & Value Stream (horizontal axis): Representing evolution over time
- Hierarchy Levels (depth axis): Representing scale from products to connected enterprises
The visual mental model resembles a three dimensional layer model or grid. Any element can be located by specifying its coordinates on these axes. A sensor’s OPC UA communication function at the work center level during the production phase occupies a specific position within this coordinate system, distinct from an enterprise planning function at the business layer during the design phase.
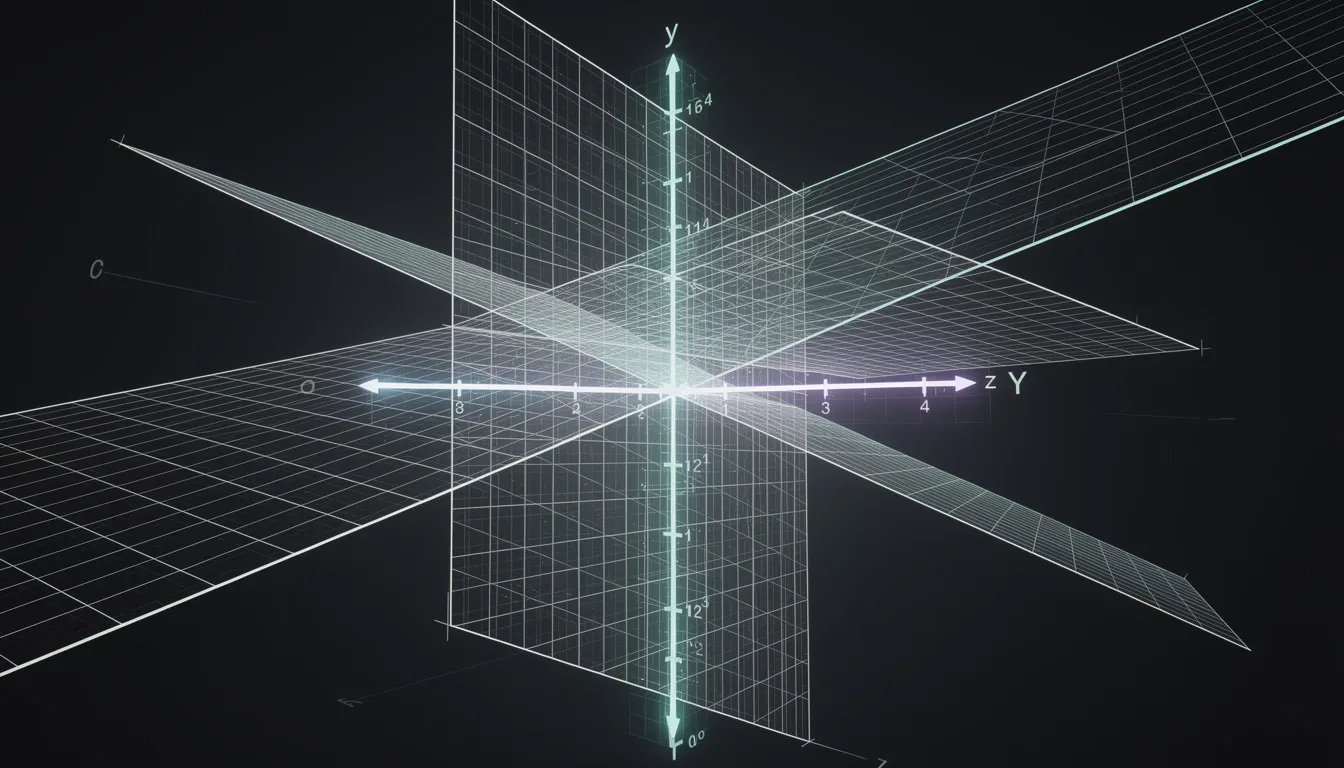
The axes are grounded in existing international standards. The Layers axis arises from IT architecture practice. The Life Cycle & Value Stream axis builds on IEC 62890 principles for life cycle and value chain management. The Hierarchy Levels axis extends IEC 62264 and ISA-95 automation levels, adding a “Product” level at the bottom and “Connected World” at the top.
The model is descriptive and classificatory. It helps organize thinking and documentation in a structured manner, but it does not prescribe how to build software, design networks, or select technologies. In Connect981’s context, RAMI 4.0 serves as a reference lens to discuss where functions like digital work instructions, traceability, and supplier collaboration would sit in a broader Industry 4.0 architecture.
Axis 1: Layers (Vertical IT Representation)
The Layers axis, sometimes called the vertical axis or left horizontal axis in certain visualizations, decomposes how a physical asset is represented and handled in IT systems. The progression moves from physical properties up through data management and business processes. RAMI 4.0 defines six layers, each with distinct responsibilities.
Asset Layer
The asset layer focuses on physical entities. These include machines, fixtures, tools, and products with their mechanical and electrical characteristics. In aerospace manufacturing, this might include a serialized composite part, a torque-controlled assembly tool, or a CNC machine. The layer encompasses the physical world, including metal parts, circuit diagrams, QR codes, and documents that represent tangible reality.
Integration Layer
The integration layer couples physical assets to the digital world. This is where sensors, controllers, fieldbus interfaces, and initial data acquisition mechanisms reside. For assets that cannot communicate on their own, such as human operators or purely mechanical components, the integration layer provides interfaces like HMIs or barcode scanners. The digital twin concept begins here, creating IT representation of physical assets.
Communication Layer
The communication layer provides standardized communication protocols and services for interoperable data transport. Examples include OPC UA, MQTT, and fieldbus gateways. This layer ensures that communication technology enables different systems to exchange data in common formats, regardless of vendor or origin.
Information Layer
The information layer structures, contextualizes, and assigns semantic meaning to raw communication data. Data management practices ensure consistent interpretation across systems. Quality attributes, maintenance histories, and production parameters receive formal definitions at this level, supporting semantic interoperability essential for smart manufacturing.
Functional Layer
The functional layer defines services, logic, and behaviors. Functions like routing selection, condition monitoring, predictive maintenance rules, and quality check logic reside here. Formal function descriptions support decision logic execution and service-oriented architecture patterns.
Business Layer
The business layer models organizational business processes, compliance rules, and economic decisions. In aerospace contexts, requirements from AS9100, FAA, or ITAR regulations would be represented at this level. The layer links manufacturing processes to legal, regulatory, and business objectives, operating above purely technical implementation.
The Layers axis separates concerns, allowing standards and solutions to focus on specific layers while still fitting into a coherent whole. This supports loose coupling between layers while maintaining high cohesion within each layer.
Axis 2: Life Cycle & Value Stream (Horizontal Development and Operation)
The right horizontal axis, or Life Cycle & Value Stream axis, captures an asset’s evolution over time. It spans from initial concept through end-of-life and distinguishes between “Type” and “Instance” perspectives.
Type Perspective
The Type perspective addresses generic product definitions, master data, and design models handled before any specific physical instance exists. In aerospace, this might include:
- A generic engine bracket specification with defined tolerances
- Master work instructions for a recurring assembly process
- Design models for prototype production before first article inspection
Type information represents blueprints and templates that define what something should be.
Instance Perspective
The Instance perspective tracks concrete physical items, batches, or machines once produced and deployed. This includes:
- Serial numbers for individual components
- Maintenance records for specific engines
- Modification histories for a particular aircraft
Instance information represents specific realizations of Type definitions.
IEC 62890 provides the foundational standard for life cycle management. RAMI 4.0 overlays Industry 4.0 concepts, such as digital twins, onto this time dimension. The axis also encompasses value stream staging from development and prototyping through production, operation, service/maintenance, and decommissioning.
For aerospace and MRO operations, this distinction matters when discussing traceability. First article inspection relates to validating that an Instance meets its Type definition. MRO overhaul processes track Instance-specific histories against Type-level requirements. The axis does not define individual process steps but provides a comprehensive framework for discussing which life cycle phase a given function or data set relates to.
Axis 3: Hierarchy Levels (Depth Across Industrial Scale)
The left horizontal axis represents hierarchy levels, expanding traditional automation levels from IEC 62264 and ISA-95 to reflect modern, connected manufacturing environments. Where traditional models stopped at the enterprise level, RAMI 4.0 extends in both directions.
Level
Description
Aerospace Example
Product
Smart products or parts with embedded identification
Serialized aerospace component with RFID tag
Field Device
Sensors, actuators, and drives interacting with physical processes
Torque sensors on assembly tools, temperature probes in curing ovens
Control Device
PLCs, CNC controllers, motion controllers orchestrating field devices
CNC controller for a 5-axis milling machine
Station
Individual machines, workstations, or inspection cells
Assembly station, automated optical inspection cell
Work Centers
Collections of stations forming process areas
Composite layup area, wing assembly line segment
Enterprise
ERP, PLM, and corporate planning systems
Multi-site production planning, quality management systems
Connected World
External networks including customers, regulators, and suppliers
Supplier data portals, regulatory submission systems
The “Product” level at the bottom is a significant extension from traditional ISA-95. It recognizes that smart products can actively influence manufacturing processes through embedded sensors or self-optimizing capabilities. This reflects the industrie 4.0 vision where products carry their own production requirements and quality data.
The “Connected World” level at the top extends beyond enterprise boundaries. In aerospace, this includes interactions with customers, regulatory bodies, and multi-tier suppliers through standards-based interfaces and shared services. The hierarchy levels represent the spectrum from individual components to global supply chain ecosystems.
Unlike rigid pyramidal hierarchies of earlier models, RAMI 4.0 assumes cross-level communication and more dynamic interactions. Components at any level can potentially communicate with other components, supporting the network-structured architectures that characterize smart factories.
Purpose and Use of Reference Architecture Models in Industry 4.0
A reference architecture model is an abstract, standardized way of describing system structures and relationships, independent of particular products. Reference models serve several important aspects in complex systems environments.
Shared Vocabulary
Reference architectures provide a neutral, agreed-upon terminology for engineers, software vendors, and policy makers. When stakeholders discuss “where” a function belongs, a reference model gives them common understanding. The hierarchy levels, layers, and life cycle phases provide a structured approach for cross-disciplinary dialogue.
Classification
Existing standards, technologies, and use cases can be mapped to specific segments of the model. This clarifies where overlaps or gaps exist. For example, OPC UA clearly maps to the Communication layer, while IEC 62890 informs the Life Cycle axis. This classification supports step by step migration from legacy systems to smart manufacturing environments.
Alignment
In complex, multi-partner ecosystems such as aerospace value chain networks, different stakeholders need common perspective on system architecture. A reference model helps align expectations and documentation without requiring every party to use identical products or platforms.
Analysis
Systematic analysis becomes possible by locating elements along the three axes and assessing interactions or dependencies. Questions like “what happens when a field device needs to communicate with enterprise systems?” can be discussed using the model’s structure.
Reference architectures like RAMI 4.0 do not mandate specific products, communication protocols, or platforms. They provide a standardized framework into which solutions can be placed. For platforms like Connect981, reference models inform conceptual discussions about where digital work instructions, traceability functions, or supplier collaboration portals sit in relation to broader Industry 4.0 structures.
RAMI 4.0 in Relation to Other Industry 4.0 Architectures
Multiple reference models coexist in the Industry 4.0 landscape. Understanding their relationships helps clarify RAMI 4.0’s specific focus.
The Industrial Internet Reference Architecture (IIRA), developed by the Industrial Internet Consortium, is domain-independent. It covers a broad range of IIoT use cases beyond manufacturing, including energy, transportation, and healthcare. The IIRA addresses a connected world of industrial applications without the specific manufacturing focus of RAMI 4.0.
Aspect
RAMI 4.0
IIRA
Primary Focus
Manufacturing, industrial production
Broad IIoT across sectors
Geographic Origin
Germany, European standardization
International, US-based consortium
Life Cycle Integration
Explicit axis based on IEC 62890
Less explicit lifecycle dimension
Hierarchy Model
Extended ISA-95 with Product and Connected World
Different functional domains approach
International organizations have also developed related frameworks. NIST’s CPS Framework addresses cyber physical systems more broadly. Sector-specific models exist for particular industries. Sometimes mappings are created to translate between these architectures.
Multiple reference models can be used in parallel. An organization might use IIRA for high-level IIoT planning and RAMI 4.0 to describe detailed manufacturing asset interactions. These models are abstract tools for structuring thought and documentation rather than prescriptive roadmaps for digital transformation or technology selection.
Conceptual Strengths and Limitations of RAMI 4.0
Strengths
RAMI 4.0 provides several conceptual benefits:
- Systematic Structure: The three-axis approach forces stakeholders to specify where, in terms of layers, life cycle phases, and hierarchy levels, a given concept belongs
- Standards Grounding: Building on established IEC standards gives the model credibility and integration with existing industrial process measurement and automation frameworks
- Cross-Disciplinary Dialogue: IT, OT, and business stakeholders can use the same coordinate system to discuss complex systems
- Neutral Framework: Technology-agnostic positioning allows the model to remain relevant as emerging technologies and artificial intelligence capabilities evolve
Limitations
Any architectural abstraction carries inherent limitations. RAMI 4.0 is no exception.
Abstraction Gap: High-level models cannot capture all real-world constraints. Legacy system quirks, specific aerospace regulations, organizational culture, and machine learning integration challenges do not map neatly onto a three-dimensional cube. The gap between model and reality requires additional guidance.
Static Representation: The model is largely static and structural. Industry 4.0 systems often exhibit dynamic, adaptive behaviors. Real-time reconfiguration, autonomous decision-making by control systems, and event-driven architectures are difficult to express in a static coordinate system.
Interpretation Variability: Organizations may interpret axes and levels differently. What one company considers a “Work Center” another might classify as a “Station.” This leads to inconsistent mappings and the need for supplementary documentation.
Scope Boundaries: RAMI 4.0 focuses on industrial production. It does not, by itself, fully address service operations, logistics networks, or detailed cybersecurity models. Other components of a complete Industry 4.0 strategy require additional frameworks.
RAMI 4.0 should be seen as one analytical lens among several. It structures discussions and documentation effectively but is insufficient on its own to fully specify or guarantee a working Industry 4.0 system. The model identifies where standards and business models might apply but does not resolve all practical challenges of integration.
Implications for Digital Industrial Operations (Without Prescriptive Guidance)
For domains like aerospace manufacturing and MRO, a model like RAMI 4.0 can inform thinking without dictating solutions.
The Layers axis offers a way to discuss where capabilities typically reside:
- Digital work instructions might span the Information and Functional layers, providing structured data with associated business logic
- Traceability functions operate across Integration, Information, and Business layers, linking physical assets to semantic data and compliance requirements
- Quality checks engage Functional layer logic with Business layer rules
The Life Cycle & Value Stream axis clarifies whether a given data set or function relates to Type or Instance information. Tracking serialized aerospace components across manufacturing and MRO requires distinguishing between master definitions and instance-specific histories. This distinction matters for data management strategies and audit requirements.
The Hierarchy Levels axis provides vocabulary for indicating whether a function pertains to field devices, stations, work centers, or enterprise and connected world levels. Multi-site coordination and supplier collaboration involve enterprise and connected world interactions, while shopfloor execution focuses on station and work center levels.
For platforms like Connect981, RAMI 4.0 acts as a reference backdrop for analysis and communication with stakeholders. When discussing how digital work instructions, traceability, and supplier portals function, the model provides a common language. However, the model does not directly define software modules, integration patterns, or deployment approaches.
RAMI 4.0 is most valuable as a conceptual reference architecture. It structures how Industry 4.0 scenarios are described and reasoned about in various industries. Practical system design requires additional, more detailed models and decisions beyond the scope of what any single reference architecture can provide. For aerospace and MRO organizations navigating Industry 4.0 concepts, the model offers a starting point for structured discussions rather than a destination.
For organizations seeking practical aerospace operations platforms that address shopfloor execution, traceability, and supplier collaboration, Connect981 offers a demo to explore how these capabilities work in real manufacturing environments.
Frequently asked questions
At its core, Industry 4.0 is about using connected, data-driven, and increasingly autonomous technologies to coordinate people, equipment, and processes across the value stream, in (near) real time.
Practically, that means:
In practice, this connects to data mapping and system interoperability when teams need to turn the answer into repeatable execution habits.
- Instrumentation of assets and processes with sensors and software to generate usable data.
- Reliable connectivity so machines, systems, and applications can exchange that data.
- Analytics and automation that turn data into concrete actions: guiding operators, adjusting equipment, or triggering workflows.
- End-to-end visibility across design, planning, production, quality, and service, not just inside a single cell or line.
How this plays out in regulated, brownfield plants
In regulated, long-lifecycle environments, Industry 4.0 almost never means ripping out MES, ERP, QMS, or validated equipment. Full replacement strategies usually fail because of qualification and validation burden, downtime risk, integration complexity, and the need to preserve traceability and change history.
Instead, the main Industry 4.0 concept shows up as:
- Layering modern connectivity and data pipelines on top of existing machines and systems.
- Integrating OT and IT data (e.g., machines, MES, QMS, PLM, ERP) so you can see and act on the same truth.
- Introducing new analytics or decision-support tools under change control and validation, without disturbing qualified baselines.
- Automating narrow, high-value workflows first (e.g., traceability, deviation response, maintenance triggers) rather than attempting a “smart factory” overhaul.
The concept remains simple: use connected data and selective automation to improve quality, throughput, and responsiveness. The execution is constrained by validation, coexistence with legacy systems, and the need for documented, traceable change.
There is no single standard number of layers for an Industry 4.0 architecture. In practice, you will see credible models ranging from about 4 to 7 layers, depending on how much separation they make between control, execution, analytics, and business functions.
Common layer counts you will see
Most Industry 4.0 reference architectures in manufacturing fall into one of these patterns:
- 4–5 layers: A compact view that groups similar concerns together. For example:
- Physical layer (machines, sensors, PLCs)
- Connectivity / data acquisition layer (gateways, OPC UA, MQTT, historians)
- Operations / execution layer (MES, SCADA, scheduling)
- Analytics / application layer (dashboards, AI/ML, optimization tools)
- Enterprise / business layer (ERP, PLM, QMS, finance)
- 6–7 layers: A more granular model that separates control vs supervision, storage vs analytics, or on-prem vs cloud. This is closer to many ISA-95 inspired stacks.
The exact number is less important than having clear responsibilities, ownership, and interfaces between layers.
How this fits with existing ISA-95 / brownfield stacks
In regulated and long-lifecycle environments, most plants already have an implicit multi-layer stack driven by ISA-95 concepts:
- Level 0–1: Field devices, drives, sensors, actuators
- Level 2: Control and supervision (PLC, DCS, SCADA, HMI)
- Level 3: Manufacturing operations (MES, LIMS, APS, data historians)
- Level 4: Business planning (ERP, PLM, QMS, SCM)
“Industry 4.0” initiatives usually add or refine layers around connectivity, data integration, and analytics on top of this, rather than replacing it. For example, you might add a dedicated data integration and analytics layer between Level 3 and Level 4, or as a cross-cutting layer alongside them.
Why you should not fixate on a specific number
- Brownfield reality: Legacy MES, SCADA, historians, and custom integrations rarely fit cleanly into textbook layers. Forcing a 5- or 7-layer picture can hide real interfaces and risks.
- Vendor architectures differ: Some vendors bundle multiple layers into one platform (e.g., connectivity + historian + analytics). Others separate them. Your logical architecture can still define separate layers even if a single product spans several.
- Regulated constraints: Splitting functionality into more layers can improve traceability and change control, but also increases validation scope and integration complexity. Fewer layers can simplify validation but may blur responsibilities.
- Lifecycle and downtime: Highly granular architectures with many layers are harder to migrate and requalify. Plants with strict uptime and qualification constraints often adopt a pragmatic subset of layers and evolve incrementally.
Practical guidance
For most regulated manufacturing environments:
- Expect to work with a 4–7 layer logical model, aligned with ISA-95 levels plus explicit data/analytics capabilities.
- Document each layer’s responsibilities, systems, data flows, and change-control boundaries.
- Be explicit where a single product spans multiple layers (for example, an MES that also acts as a data hub or scheduling engine).
- Plan Industry 4.0 additions as coexisting layers or services on top of existing MES/ERP/SCADA, not as full replacements, unless you have a clear path to requalification, minimal downtime, and controlled migration.
In summary, a “typical” Industry 4.0 architecture in manufacturing is best described as a 4–7 layer reference model adapted to your existing stack, rather than a fixed, standard layer count.
Industry 4.0 is a shorthand for using connected, data-driven technologies to run manufacturing and supply chains more intelligently. In simple terms, it is:
“Connecting machines, people, and systems so data flows in real time and software can help decide what to do next.”
In practice, this connects to data mapping and system interoperability when teams need to turn the answer into repeatable execution habits.
Core ideas in practical terms
In an industrial, regulated environment, Industry 4.0 usually shows up as:
- Connected equipment: Machines, tools, and sensors that send data (status, parameters, alarms, usage) into your plant network and systems.
- Integrated systems: MES, ERP, QMS, PLCs, historians, and lab systems exchanging data instead of living in silos.
- Digital workflows: Work instructions, deviations, approvals, and change records managed in software with traceability.
- Analytics and automation: Using collected data for monitoring, forecasting, optimization, or closing certain loops automatically (with defined limits and controls).
- Human-in-the-loop decisions: Operators, supervisors, quality, and engineering getting better, more-timely information rather than being replaced.
What Industry 4.0 is not
- It is not a single product you can buy. It is a combination of technologies and process changes.
- It is not a guarantee of compliance, audit success, or safety. Those still depend on process design, validation, and governance.
- It is not an overnight “smart factory” transformation. In brownfield plants, progress is incremental and constrained by legacy systems and qualification requirements.
How this works in a brownfield, regulated plant
In most regulated and long-lifecycle environments, Industry 4.0 looks like layering capabilities onto what you already have, for example:
- Adding condition monitoring sensors to legacy machines instead of replacing the machines.
- Integrating MES with QMS and ERP so deviations, lots, and orders line up automatically.
- Replacing paper travelers and work instructions with digital versions tied to revision control and electronic signatures.
- Using a historian or data platform to combine process data, quality results, and maintenance history for analysis.
Full replacement strategies often fail or stall because they require long downtime, re-validation of entire lines, retraining, and re-integration with existing systems. As a result, most plants pursue Industry 4.0 as a controlled, stepwise program rather than a single big-bang change.
Key constraints and tradeoffs
- Traceability and validation: Any new digital connection or automation that affects product or records must be validated and governed under change control.
- Integration complexity: Connecting multiple vendors’ MES/ERP/QMS/PLM systems and legacy equipment can be harder than deploying the new tool itself.
- Downtime risk: Aggressive upgrades or replacements can threaten output commitments and regulatory commitments if they fail.
- Data readiness: Benefits from advanced analytics or AI depend on data completeness, quality, and clear ownership. Many plants need basic data hygiene before advanced use cases pay off.
In simple terms: Industry 4.0 is about making your existing manufacturing system more connected, observable, and data-driven, under the realities of regulation, validation, and long-lived assets.
An Industry 4.0 course is a structured training program that explains how digital technologies are applied in manufacturing and industrial operations. In practice, it should cover how connectivity, data, analytics, and automation change day-to-day work in production, quality, and engineering, not just buzzwords like IoT or AI.
Typical topics in an Industry 4.0 course
Most courses will address some mix of:
In practice, this connects to a connected execution platform when teams need to turn the answer into repeatable execution habits.
- Connectivity and data collection: Industrial networking basics, OPC UA, IIoT gateways, historian concepts, and how to extract data from CNCs, PLCs, test stands, and legacy cells.
- Data platforms and integration: How shop-floor data can be linked to MES, ERP, QMS, PLM, and LIMS, and why integration architecture and master data quality matter.
- Analytics and AI: Use of dashboards, OEE analytics, anomaly detection, predictive maintenance, and limitations when data is sparse, noisy, or unstructured.
- Digital workflows: Electronic work instructions, eDHR/eBR, digital logbooks, defect capture, and basic concepts like traceability and genealogy.
- Automation and cyber-physical systems: Collaborative robots, automated material handling, and how they interact with safety systems and quality controls.
- Cloud and edge computing: Tradeoffs between running workloads on-premises vs in the cloud, with attention to latency, security, and plant IT constraints.
- Change management and organization: Skills, roles, and governance needed to make digital projects stick rather than remain pilots.
What matters in regulated, brownfield environments
For aerospace, medical, defense, or similar regulated sectors, a generic Industry 4.0 course is often too optimistic or greenfield-focused. To be practically useful, it should explicitly address:
- Validation and qualification impact: How new digital tools affect equipment qualification, software validation, and documented testing. A course should not imply that any technology is “compliant” by default.
- Change control and traceability: How configuration changes to MES, data pipelines, or analytics models are controlled, documented, and traceable over long asset lifecycles.
- System coexistence: Strategies for layering new capabilities on top of legacy MES/ERP/QMS/PLM rather than trying to rip and replace, given downtime, integration, and requalification risks.
- Data integrity and auditability: How timestamps, user attribution, versioning, and access control are handled so that digital records can support investigations and audits.
- Cybersecurity in OT: Alignment with plant security controls, segmentation, remote access policies, and how to avoid introducing unmanaged devices on the network.
- Lifecycle planning: The reality that equipment, test systems, and validated software may stay in use for 10–20+ years, so solutions must accommodate that horizon.
Different types of Industry 4.0 courses
Depending on the audience, courses may be structured as:
- Executive or leadership overviews: Focused on strategy, portfolio selection, and governance. Useful for deciding where Industry 4.0 actually fits the plant roadmap.
- Technical deep dives: For OT/IT, process engineers, and data teams, covering architectures, protocols, reference designs, and common failure modes.
- Operations-focused training: Aimed at supervisors and engineers, centered on concrete use cases like digital work instructions, NCM management, OEE, and line monitoring.
- Vendor-specific programs: Training around a particular platform or product. These can be helpful but are often biased toward idealized implementations and may not fully cover integration, validation, or coexistence issues.
How to assess whether a course is actually useful
For plants with complex legacy systems and regulatory expectations, an Industry 4.0 course is more credible if it:
- Shows how to integrate with existing MES/ERP/QMS instead of assuming a greenfield stack.
- Discusses how to handle partial, inconsistent, or unstructured data and the impact on analytics quality.
- Addresses validation, documented testing, and change control as first-order topics, not afterthoughts.
- Uses realistic examples with constrained downtime, mixed vendors, and long-lived equipment.
- Separates what can be proven today from aspirational use cases or vendor roadmaps.
In short, an Industry 4.0 course should help your teams understand how digital tools fit your specific operational and regulatory constraints, not just teach generic concepts or promise full system replacement that is unlikely to be feasible in a brownfield, regulated environment.
Industry 4.0 and Industry 5.0 are not two separate technology stacks. They are overlapping waves of how digital technologies are applied in manufacturing. In regulated, brownfield environments, Industry 5.0 concepts typically build on Industry 4.0 capabilities rather than replace them.
Core focus: optimization vs. optimization + human-centricity
Most Industry 4.0 initiatives focus on:
In practice, this connects to a connected execution platform when teams need to turn the answer into repeatable execution habits.
- Connecting machines, sensors, and systems (MES, ERP, QMS, historians)
- Automating data capture and control (IIoT, SCADA, CNC integrations, PLC links)
- Using analytics and AI/ML to improve OEE, yield, and cost
- End-to-end traceability and genealogy
Industry 5.0 builds on this foundation but shifts emphasis to:
- Human-centric work: technologies that support, not replace, skilled operators, inspectors, and engineers (e.g., digital work instructions, AR-assisted tasks, decision support instead of black-box automation).
- Resilience: designing systems that can adapt to supply disruptions, equipment failures, workforce changes, and regulatory updates without brittle dependence on a single platform or vendor.
- Sustainability: monitoring and reducing energy use, waste, and rework, and making those tradeoffs visible in operations decisions.
Technology examples in Industry 4.0 vs. Industry 5.0
Most underlying technologies are shared. The difference is how they are applied and governed.
Common Industry 4.0 technology patterns:
- IIoT platforms collecting data from PLCs, CNC machines, test stands, and environmental monitors.
- Advanced MES capabilities: digital travelers, eDHR/eBR, integrated NC/CAPA workflows (when connected to QMS).
- Advanced analytics: OEE dashboards, predictive maintenance models, automated SPC alerts.
- Cloud or hybrid data lakes combining MES, ERP, QMS, and historian data.
Typical Industry 5.0-leaning technology uses:
- Operator-centric HMIs and digital work instructions that guide complex, high-mix operations while preserving traceability.
- Decision-support tools that keep humans in the loop for quality, release, and deviation decisions rather than fully automating them.
- Collaborative robotics that can be reconfigured by technicians without extensive reprogramming, subject to safety and validation constraints.
- Analytics that explicitly show tradeoffs between throughput, quality risk, compliance risk, and resource use (labor, energy, materials).
- Workforce knowledge capture: capturing tribal knowledge into validated procedures, checklists, or rule-based assistive tools.
In practice, the same MES, historian, or IIoT stack might underpin both Industry 4.0 and Industry 5.0 use cases. The differentiator is whether the implementation is primarily automation-centric or truly human- and resilience-centric.
Implications in regulated, brownfield environments
In aerospace, medical, defense, and similar environments, the line between Industry 4.0 and 5.0 is constrained by validation, qualification, and long equipment lifecycles.
- Brownfield reality: Existing MES, ERP, QMS, PLM, and machine controllers are not easily replaced. Industry 5.0 concepts usually come in as extensions or overlays (digital work instructions, decision support, analytics) around those systems.
- Validation and change control: Any new “smart” or assistive function that affects product quality, data integrity, or release decisions must go through validation and formal change control. That can limit how quickly AI-driven or adaptive features are deployed.
- Traceability and explainability: Human-in-the-loop decisions must be traceable. Any advanced analytics or AI introduced under an Industry 5.0 banner needs clear inputs, outputs, and justification paths that can be audited and reproduced.
- Safety and regulatory boundaries: Collaborative systems and decision-support tools cannot offload accountability from qualified personnel. Technology can recommend; people remain responsible for regulated decisions.
Where Industry 5.0 adds practical value
When separated from hype, Industry 5.0 ideas can be useful for prioritizing investments:
- Augmenting complex, high-mix, low-volume work: Digital guidance at the station that reflects current configuration, deviations, and engineering changes, and that integrates with MES/QMS for traceability.
- Supporting a changing workforce: Tools that shorten the time for new technicians to safely perform validated procedures, without weakening procedural controls.
- Building operational resilience: Architectures that keep critical operations running even if cloud services or a specific platform are unavailable, and that degrade gracefully rather than failing hard.
- Making tradeoffs visible: Dashboards and models that show quality risk, compliance risk, and rework implications, not just throughput and cost.
Key tradeoffs and pitfalls
- Overpromising “5.0” as a reset: Positioning Industry 5.0 as a clean break or a new platform to replace everything usually fails in regulated plants, given qualification burden, validation cost, downtime risk, and complex integrations.
- Underestimating integration debt: Human-centric tools still need clean, timely data from MES, ERP, QMS, and machines. Without solid integration and master data governance, “5.0” experiences quickly degrade or become untrusted.
- Black-box AI: Unexplainable AI in quality, release, or safety-critical decisions is hard to defend in audits and may not pass internal quality or regulatory review.
- Fragmented UX: Adding yet another “smart” application without aligning to existing workflows can increase cognitive load for operators, the opposite of human-centric design.
How to think about Industry 4.0 vs. 5.0 in your roadmap
For most regulated manufacturers, a practical framing is:
- Use Industry 4.0 language when focusing on connectivity, automation, and data quality across machines and systems.
- Use Industry 5.0 language when deliberately designing for human roles, resilience, and sustainability on top of that connected foundation.
In both cases, success depends less on the label and more on disciplined integration, validation, change control, and realistic alignment with existing MES/ERP/QMS and equipment lifecycles.
The RAMI 4.0 (Reference Architecture Model for Industry 4.0) model is a three-dimensional reference framework used to structure and discuss Industry 4.0 systems. It gives a common map for how assets, data, functions, and business processes relate, without prescribing a specific vendor stack or architecture.
What RAMI 4.0 is
RAMI 4.0 is a conceptual model developed mainly in the German Industry 4.0 context. It helps organizations:
In practice, this connects to data mapping and system interoperability when teams need to turn the answer into repeatable execution habits.
- Classify existing and planned systems (OT, IT, and IoT) in a consistent way.
- Identify where specific standards and interfaces apply.
- Expose gaps in integration, data ownership, and responsibilities.
- Support structured discussions between engineering, operations, IT, and suppliers.
It is especially useful in complex, regulated, brownfield environments where you need a neutral map to reason about many interacting systems and long-lived assets.
The three dimensions of RAMI 4.0
The model is typically represented as a cube with three axes:
-
Layers (vertical axis) – from physical asset up to business level:
- Asset: Physical or logical asset (machine, tool, test stand, software component).
- Integration: How assets are connected and identified (sensors, device drivers, connectivity).
- Communication: Protocols and messaging (e.g., fieldbuses, OPC UA, MQTT, IIoT platforms).
- Information: Data models, semantics, and contextualization (tags, product data, batch data, genealogy).
- Functional: Functions and services (control logic, analytics, apps, MES functions).
- Business: Enterprise processes and rules (planning, costing, compliance processes, KPIs).
-
Lifecycle & value stream (one horizontal axis)
- Ranges from initial concept and development of an asset or product through operation, maintenance, and decommissioning.
- Lets you distinguish between engineering-time activities (design, configuration) and run-time activities (production, service).
- Supports thinking about how product and asset data must persist across decades in regulated environments.
-
Hierarchy levels (other horizontal axis)
- Extends and modernizes the ISA-95 / IEC 62264 style levels.
- Includes elements such as product, field device, control device, station, work center, enterprise, and connected world.
- Helps map what lives at machine level, line level, plant level, and multi-site/cloud level.
How RAMI 4.0 is used in practice
In regulated and high-criticality environments, RAMI 4.0 is typically used as a planning and alignment tool rather than a strict implementation blueprint. Common uses include:
- Architecture inventory: Mapping existing PLCs, SCADA, MES, historians, QMS, ERP, and IIoT components onto RAMI layers and hierarchy levels to see overlaps and gaps.
- Standard alignment: Relating specific standards (e.g., OPC UA, IEC 62443, ISA-95) to parts of the model so responsibilities are clearer.
- Scope definition: Clarifying where a new project fits (for example, “Communication and Information layers at station and work-center levels”), which helps with stakeholder alignment and validation plans.
- Integration planning: Identifying where interfaces are required between legacy and new systems, and what semantics need to be harmonized.
- Governance and traceability: Structuring discussions about who owns which layer, what must be validated, and how changes are controlled over the system lifecycle.
What RAMI 4.0 is not
- Not a product or platform: You cannot buy or install RAMI 4.0. Vendors may claim “RAMI 4.0 compatibility,” but that typically means their offering can be positioned within the model or uses related standards.
- Not a detailed design: It does not replace system-level design, safety analysis, or cybersecurity architecture. It is a high-level map.
- Not a compliance guarantee: Using RAMI 4.0 does not ensure regulatory compliance, audit success, or certification. Validation, documentation, and local regulatory expectations still drive outcomes.
- Not prescriptive about migration: It does not tell you how quickly to modernize or whether to replace versus wrap legacy systems.
Implications for brownfield, regulated environments
For most established plants, RAMI 4.0 is applied retrospectively to a brownfield landscape:
- Coexistence over replacement: Mapping legacy PLCs, DCS, MES, and ERP in RAMI terms usually reinforces that full replacement is risky and costly due to validation, downtime, and traceability impacts. Incremental layering and integration is more realistic.
- Validation scope control: By clarifying which layers and hierarchy levels a change touches, RAMI 4.0 can help bound validation and qualification effort and highlight where impact is largest.
- Long lifecycle awareness: The lifecycle axis surfaces issues like how long engineering data, batch records, and configuration histories must be retained and accessible, especially when introducing cloud services or new integration technologies.
- Standards mapping: You can use RAMI 4.0 to decide where to prioritize standardization (for example, OPC UA at the Communication layer vs. common information models at the Information layer) while acknowledging constraints of existing equipment.
Key tradeoffs and limitations
- Abstraction vs. specificity: RAMI 4.0 is intentionally abstract. It helps align stakeholders, but you still need detailed engineering, cybersecurity, and validation design to make it operational.
- Interpretation differences: Different teams and vendors interpret the layers and hierarchy levels differently. Establishing site-specific conventions is important if you want consistent use.
- Effort vs. value: A full, precise mapping of every system to RAMI 4.0 can be time-consuming. Many organizations get value from using it selectively around major assets, product families, or integration projects.
- Standard evolution: The Industry 4.0 ecosystem and related standards evolve. A RAMI-based view needs periodic review to stay useful and aligned with current technologies and regulations.
Used pragmatically, RAMI 4.0 is a shared reference model that helps experienced teams think more systematically about Industry 4.0 initiatives, particularly in complex, validated, multi-vendor environments where full rip-and-replace strategies are rarely viable.
An Industry 4.0 capability model is a structured way to describe, assess, and plan the progression of a manufacturing organization from basic, mostly manual operations to highly connected, data-driven, and (selectively) automated operations. It is a conceptual framework, not a formal standard, certification, or compliance guarantee.
What the capability model is trying to capture
Most Industry 4.0 capability models describe maturity across several dimensions that matter to an industrial site, for example:
In practice, this connects to industry insight and operational thought leadership when teams need to turn the answer into repeatable execution habits.
- Data & connectivity: From islands of data in machines and spreadsheets to integrated, contextualized data across MES, ERP, QMS, historians, and shop-floor devices.
- Automation & control: From manual setups and paper-based checks to selective automation with feedback from sensor data and closed-loop control where justified.
- Analytics & decision support: From descriptive reporting to predictive and prescriptive analytics, with clear ownership and validation of models where they influence quality or safety.
- Workforce & processes: From tribal knowledge and informal workarounds to standardized digital work, traceable change control, and structured continuous improvement.
- Governance & lifecycle: From ad hoc experiments to managed portfolios of digital capabilities with defined owners, support models, and validation/qualification approaches.
The model gives you a common language to discuss where you are today and what is realistic to pursue next, given regulatory constraints, legacy systems, and limited downtime windows.
Common structure of Industry 4.0 capability models
Although different vendors and consultants publish their own versions, most models follow a similar pattern:
- Levels or stages: Typically 4 to 6 maturity levels, e.g. “basic”, “managed”, “integrated”, “optimized”, sometimes “autonomous” or “self-optimizing” at the top.
- Capability domains: Categories such as operations, quality, maintenance, supply chain, IT/OT integration, and workforce.
- Descriptors or criteria: Qualitative or semi-quantitative descriptions of what each level looks like in each domain.
Used carefully, this lets you say things like “we are at level 2 for real-time quality data, but closer to level 4 for equipment connectivity” rather than declaring a blanket maturity level for the entire site.
How capability models are used in practice
Industry 4.0 capability models are typically used to:
- Assess current state: Facilitate structured discovery across manufacturing, quality, engineering, and IT to locate gaps and duplication of effort.
- Prioritize initiatives: Focus on capabilities that remove real constraints (e.g. genealogy gaps, manual data transcription) instead of chasing generic “smart factory” milestones.
- Align stakeholders: Provide common terminology so operations, quality, and IT can discuss tradeoffs without getting locked into specific vendor products.
- Track progress: Re-assess periodically to confirm that investments are moving actual capabilities forward, not just adding dashboards or pilots.
In regulated, long-lifecycle environments, the most useful models are the ones that explicitly consider validation, change control, and the realities of multi-decade equipment and software lifespans.
Constraints and limitations
There are several important limitations to keep in mind:
- No single canonical model: There is no universally accepted “official” Industry 4.0 capability model. Different consulting firms, industry groups, and vendors publish their own. Using a model does not imply any external recognition or certification.
- Not a compliance framework: Capability models do not replace quality system requirements, regulatory guidance, or internal procedures. They do not guarantee audit outcomes or product compliance.
- Vendor bias: Some models are structured to align with a specific vendor stack. In brownfield environments with multiple MES, ERP, PLM, and QMS platforms, adopting a vendor-centric model at face value can lead to unrealistic replacement roadmaps.
- Coarse granularity: Levels are typically broad. A plant can be highly mature in one area (e.g. OEE monitoring) and low in another (e.g. electronic device history records). For planning, you usually need a more detailed, capability-by-capability view.
- Context dependence: The value of a given maturity level depends on your regulatory context, product mix, and risk profile. For example, “autonomous” optimization may be neither desirable nor justifiable for certain safety-critical processes.
How it fits with brownfield, regulated environments
In most aerospace, defense, medical device, and similar environments, the Industry 4.0 capability model should be applied with the following realities in mind:
- Coexistence, not wholesale replacement: Moving from a lower to a higher maturity level rarely means replacing MES, ERP, PLM, or QMS outright. Full replacement often fails due to qualification and validation effort, downtime risk, integration complexity, and the need to preserve historical traceability.
- Incremental upgrades: Real progress usually comes from targeted capabilities layered on existing systems: better data integration, improved genealogy capture, digital work instructions, or more robust evidence management, rather than large-bang platform swaps.
- Validation and change control: Any capability that affects product realization, release, or records must pass through defined validation and change processes. A maturity model can help you choose a sequence of improvements that fits your validation capacity.
- Long equipment lifecycles: Many machines and control systems will not be replaced to achieve higher “levels” of Industry 4.0. Instead, you wrap them with connectivity, data collection, and procedural controls that move your overall capability forward while keeping qualified assets in place.
Practical way to use an Industry 4.0 capability model
For a plant leadership team, a pragmatic approach is:
- Select or adapt a model that explicitly includes data integration, traceability, and governance, not just automation and AI.
- Assess current state by capability domain, involving operations, quality, engineering, and IT.
- Map findings onto existing systems and constraints: which gaps are blocked by legacy systems, validation burden, or downtime limits.
- Define a small number of high-impact, low-regret capability steps (for example, improving evidence capture for audits, or reducing manual data entry between systems).
- Plan these steps as controlled changes, with clear owners, success criteria, and alignment with existing qualification and validation practices.
Used this way, the Industry 4.0 capability model becomes a planning and communication tool, not a promise of a particular technology stack or a shortcut to compliance.
An Industry 4.0 maturity model is a structured framework for assessing how far an organization has progressed in adopting digital, connected, and data-driven capabilities in manufacturing. It breaks that progress into levels and dimensions so you can benchmark your current state, identify realistic next steps, and prioritize investments.
What the model typically covers
Most Industry 4.0 maturity models share a few common elements, even if the labels differ by vendor or consulting firm:
In practice, this connects to industry insight and operational thought leadership when teams need to turn the answer into repeatable execution habits.
- Levels of maturity: A staged path from basic, manual practices toward increasingly integrated, automated, and data-driven operations.
- Multiple dimensions: Separate views of technology, data, processes, people/organization, and governance.
- Assessment criteria: Qualitative or quantitative questions used to score a plant, line, or function against each dimension.
- Roadmapping guidance: Suggested next steps for moving from one level to the next, often tied to specific use cases (e.g., OEE analytics, digital work instructions, advanced scheduling).
Typical levels in an Industry 4.0 maturity model
Naming varies, but many models can be roughly mapped to the following pattern:
- Level 1: Basic / Manual
Paper-based travelers, spreadsheets, and standalone machines. Data collection is manual and inconsistent. Little to no real-time visibility. Improvements rely on local expertise and tribal knowledge. - Level 2: Digitized
Documents and records (work instructions, batch records, quality logs) are digital, but systems are siloed. Basic MES, LIMS, or QMS may exist, often with manual re-entry between systems. Reporting is largely historical. - Level 3: Connected
Key systems (MES, ERP, QMS, SCADA, historians) are partially integrated. Machine and process data flows automatically into central repositories. Operators and engineers have near real-time dashboards for OEE, scrap, and downtime. - Level 4: Predictive / Optimized
Advanced analytics, modeling, and automated decision support (e.g., predictive maintenance, statistical process control with alerts, optimization of schedules or recipes). Feedback loops exist from quality and field performance back into design and process engineering. - Level 5: Adaptive / Autonomous
Highly orchestrated, self-optimizing systems where many decisions (e.g., parameter tuning within validated ranges, dynamic routing) are made automatically under defined governance and oversight. Humans focus on supervision, exception handling, and continuous improvement.
These levels are conceptual; in practice, most regulated plants sit at different levels for different areas (e.g., Level 3 for data collection/OEE, Level 2 for quality documentation, Level 1 for some legacy equipment).
Key dimensions relevant in regulated, brownfield environments
A useful Industry 4.0 maturity model for regulated manufacturing usually considers at least the following dimensions:
- Technology & automation: Extent of sensors, connectivity (e.g., OPC UA, fieldbus, custom interfaces), robotics, and automation. In brownfield sites, this is constrained by legacy controllers, proprietary protocols, and limited downtime windows.
- Data & integration: How data is collected, contextualized, and integrated across MES, ERP, QMS, PLM, historians, and shop-floor systems. Incomplete integration, custom middleware, and interface fragility are common limiting factors.
- Process & standard work: Degree to which processes are standardized, documented, and measured. Digital work instructions, electronic batch records, and structured deviation/CAPA workflows are key markers of maturity.
- Quality & traceability: Depth and reliability of genealogy, event logging, and evidence management. Higher maturity implies traceability by design, not as an after-the-fact reporting problem.
- Organization & skills: Operator and engineer familiarity with digital tools, data literacy, and the presence of cross-functional teams (operations, quality, IT/OT) to manage change and address failures.
- Governance, validation & change control: How rigorously changes to systems are specified, tested, documented, and validated. In regulated environments, this dimension often limits the pace of Industry 4.0 initiatives more than technology itself.
What the maturity model is (and is not) useful for
Used appropriately, an Industry 4.0 maturity model can help you:
- Establish a common language between operations, engineering, quality, and IT about the current state and priorities.
- Prioritize investments by focusing on a small number of high-impact, feasible next steps rather than chasing a fully autonomous vision.
- Avoid overreach by recognizing gaps in data, validation, and change control that would undermine more advanced use cases.
- Compare sites sensibly while still accounting for local regulatory requirements, product mix, and equipment age.
It is not:
- A compliance standard or certification.
- A guarantee that a given level of maturity will pass an audit or satisfy regulators.
- A justification on its own for ripping and replacing legacy systems.
- A linear checklist where every plant must reach Level 5; for many regulated operations, an optimized, well-governed Level 3–4 in key areas is both realistic and sufficient.
Tradeoffs and constraints in regulated, long-lifecycle environments
In aerospace, medical, defense, and similar sectors, the path up the maturity model is shaped heavily by constraints that generic 4.0 diagrams often gloss over:
- Qualification and validation burden: Any significant change to MES, batch records, control logic, or data flows may trigger requalification and revalidation. This adds time, cost, and documentation overhead that must be factored into the roadmap.
- Downtime risk: Connecting or upgrading legacy equipment can require outages that are difficult to schedule. Many sites can only make incremental changes during short maintenance windows.
- Integration complexity: Existing MES/ERP/QMS stacks often use custom integrations built over many years. Replacing them fully to “jump” maturity levels can introduce serious risk to traceability, data integrity, and on-time delivery.
- Traceability and evidence expectations: Any step up in automation or analytics must maintain or improve evidence trails. If a solution complicates auditability or change tracking, it will stall regardless of its theoretical maturity benefit.
Because of these constraints, full replacement strategies intended to leap directly to high Industry 4.0 maturity often fail or are abandoned. Incremental coexistence, wrapping and extending existing systems, and targeting specific use cases (e.g., improved OEE visibility, electronic logbooks, or better deviation management) tend to be more realistic.
How to use a maturity model practically
To make an Industry 4.0 maturity model actionable in your context:
- Define the scope: Decide whether you are assessing a single line, a plant, or a function (e.g., quality management). Trying to score everything at once usually obscures critical detail.
- Use cross-functional input: Include operations, maintenance, quality, IT/OT, and planning. Many self-assessments fail because they only capture one perspective.
- Score honestly and simply: Use a coarse scale (e.g., 1–5) and focus on representative evidence (current systems, procedures, reports) instead of aspirational descriptions.
- Identify 3–5 realistic next steps: For example, standardizing data collection for downtime, digitizing specific paper forms, or integrating existing MES and QMS for deviations.
- Align with validation and change control: Treat each maturity step as a change project that must be specified, risk-assessed, tested, documented, and, where required, validated.
- Iterate regularly: Revisit the maturity assessment after significant changes or on a fixed cadence to adjust priorities as constraints and capabilities evolve.
Connecting this to your environment
In a typical brownfield, regulated plant, your Industry 4.0 maturity will not be uniform across the organization. Rather than chasing a generic “Level 5,” use the maturity model to highlight where incremental changes in integration, digital work instructions, traceability, or analytics can deliver measurable operational and quality benefits while staying within your validation and downtime constraints.
There is no single, universally accepted “Industry 4.0 certification” in the way there is, for example, a specific ISO standard certificate. What exists today is a mix of:
- Vendor or consultancy “Industry 4.0 ready” badges and assessments
- National or regional programs that assess digital maturity
- Certificates for specific enabling technologies (cybersecurity, connectivity, cloud, etc.) that are sometimes marketed as Industry 4.0 related
These can be useful maturity or capability indicators, but they do not constitute a universal regulatory or audit guarantee, and they are not interchangeable.
What people usually mean by Industry 4.0 certification
In practice, when organizations talk about Industry 4.0 certification, they usually mean one of the following:
- Digital maturity assessments: A structured evaluation of how far a plant has progressed on connectivity, data usage, automation, analytics, and organizational readiness.
- Vendor solution certifications: A supplier certifies that its equipment or software supports certain protocols or interoperability features often associated with Industry 4.0.
- Training or personnel certificates: Courses that certify individuals in Industry 4.0 concepts, architectures, or implementation methods.
- Framework-aligned labels: Some industry bodies or regional initiatives publish criteria and issue labels (for example, for smart factory or digital production) that many people loosely call Industry 4.0 certs.
None of these is a globally harmonized, one-size-fits-all certification. Their scope, rigor, and recognition vary widely.
How this relates to regulated manufacturing
In regulated and long-lifecycle environments, Industry 4.0-oriented certifications should be treated as inputs to your own governance, not as proof of compliance. In particular:
- No compliance guarantee: An Industry 4.0 label does not replace ISO 9001, IATF 16949, AS9100, FDA expectations, or any sector-specific requirements.
- No shortcut to validation: Even if a solution is marketed as Industry 4.0 certified, you still need to perform your own validation, integration testing, risk assessment, and change control.
- Traceability still local: Audit trails, data integrity, and genealogy must be demonstrated in your own environment, with your configurations and processes. Third-party certificates rarely address this level of detail.
- Brownfield constraints: Many Industry 4.0 assessment schemes assume a relatively greenfield or homogeneous stack. In reality, legacy MES, ERP, PLM, QMS, and bespoke integrations often limit how far you can adopt a reference model without major qualification and downtime risk.
Where Industry 4.0-oriented certifications can be useful
Despite their limitations, these certifications and assessments can be helpful if used carefully:
- As a structured maturity framework: A formal Industry 4.0 assessment can help benchmark sites, identify obvious gaps (for example, lack of standardized data models or manual data collection), and prioritize investments.
- As procurement input: Vendor declarations and certifications around interoperability, cybersecurity, and open interfaces can help narrow options, provided they are verified and aligned with your architecture and validation practices.
- As internal communication tools: Using a recognized framework can help align operations, IT, and quality around a shared roadmap and terminology for digitalization.
To extract real value, you need to map any Industry 4.0 criteria to your own requirements, regulatory context, and lifecycle constraints.
Key tradeoffs and failure modes
There are some common pitfalls in relying on Industry 4.0 certifications in industrial operations:
- Overreliance on badges: Treating a vendor or plant badge as proof of compliance, instead of verifying data integrity, process controls, and configuration in your own environment.
- Full replacement assumptions: Some Industry 4.0 narratives imply ripping and replacing legacy MES/QMS/ERP to reach a target state. In aerospace-grade or similar environments, this is often impractical due to validation cost, downtime risk, and integration complexity.
- Ignoring integration debt: Certifications often look at point capabilities, not how well systems interoperate in a brownfield context where old and new platforms must coexist for years.
- Insufficient traceability: Assessments may focus on connectivity and analytics, while auditors will focus on traceability, data lineage, and change control, which depend heavily on local implementation details.
How to evaluate Industry 4.0 certification offers
If you are considering an Industry 4.0 certification or maturity assessment, it is useful to ask:
- Who recognizes this certification and in what context (industry body, region, specific OEMs)?
- What exact domains does it cover (connectivity, cybersecurity, data governance, analytics, organization, skills)?
- Does it explicitly address regulated environments, validation, and traceability, or is it generic?
- How does it treat legacy systems and long qualification cycles?
- Can its criteria be mapped to our internal requirements and risk models?
- What evidence and documentation are generated that we can reuse for audits or internal governance?
For most regulated manufacturers, the most practical approach is to treat Industry 4.0 certification frameworks as structured checklists or reference models to inform your own roadmap and internal standards, rather than as end goals or proof of compliance.
Bottom line
Industry 4.0 certification is not a single standardized credential. It usually refers to vendor programs, maturity models, or training certificates related to digital manufacturing. In regulated, brownfield environments, it can be a useful input to strategy and design, but it does not remove the need for plant-specific validation, integration work, and robust change control.
Industry 4.0 architecture is a layered approach to how machines, control systems, data platforms, and enterprise applications are connected so that production data can be collected, contextualized, analyzed, and used to drive decisions and automation. It is not a single product or standard. It is the target structure of your OT/IT landscape that enables modern capabilities like real-time visibility, predictive maintenance, advanced traceability, and closed-loop quality.
Typical layers in an Industry 4.0 architecture
Names differ by vendor and plant, but most architectures include the following functional layers:
In practice, this connects to data mapping and system interoperability when teams need to turn the answer into repeatable execution habits.
- Physical & field level: Machines, robots, sensors, actuators, tooling, test equipment, gauges, and manual stations. In regulated plants this often includes long-lived qualified equipment that cannot be casually swapped or significantly modified.
- Control & automation level: PLCs, CNC controllers, DCS, SCADA, and safety systems. These execute real-time control and are typically validated and governed by strict change control in pharma, aerospace, and medical devices.
- Operations management level: MES, LIMS, WMS, CMMS/EAM, SPC systems, historian, and sometimes QMS modules operating near the shop floor. This is where execution logic, genealogy, electronic batch records, and routing logic often live.
- Enterprise applications level: ERP, PLM, QMS, APS, and SCM systems that manage orders, bills of material, design data, quality records, and planning. Changes here can impact traceability, financials, and regulatory evidence.
- Data & analytics level: Data lakes, data warehouses, historian replicas, IIoT platforms, analytics engines, dashboards, and AI/ML pipelines. This layer aggregates and contextualizes data from multiple systems for monitoring, optimization, and engineering studies.
- Access & interaction level: Web portals, operator UIs, mobile apps, digital work instructions, engineering dashboards, and APIs that users and external systems rely on.
An Industry 4.0 architecture defines how these layers interconnect, what data moves between them, and through which interfaces and protocols.
Key architectural principles
Most Industry 4.0 architectures in regulated manufacturing aim for:
- Standardized connectivity: Use of industrial protocols and integration standards (for example, OPC UA, MQTT, REST APIs, message queues) instead of one-off point-to-point interfaces. In brownfield plants, gateways or edge devices often bridge legacy protocols.
- Separation of concerns: Keeping real-time control separate from analytics and experimentation, to avoid jeopardizing safety, validation status, or uptime.
- Data contextualization: Associating raw signals with products, batches, operations, materials, tooling, and workers so that data is usable for quality, compliance, and engineering, not just for monitoring.
- Traceability and auditability: Ensuring that data flows and transformations can be traced, versioned, and justified, which is essential when data is used as evidence in audits or investigations.
- Security and segmentation: Network zoning and role-based access control that align OT and IT cybersecurity with regulatory expectations, while still allowing needed data sharing.
- Extensibility: The ability to add new equipment, analytics use cases, or external partners without a major redesign every time.
Brownfield reality: coexistence, not wholesale replacement
In most regulated and high-criticality environments, Industry 4.0 architecture is an overlay and re-organization of existing systems, not a greenfield replacement. Full rip-and-replace strategies frequently fail or stall because of:
- Qualification and validation burden: Replacing MES, ERP, or major automation platforms can trigger extensive validation and requalification, including re-running PQ/OQ, updating procedures, and re-training operators.
- Downtime risk: Long outages to switch core systems are often unacceptable when there are tight delivery commitments, limited alternate capacity, or contractual service levels.
- Integration complexity: Legacy MES/ERP/QMS stacks often have many hidden integrations built over years. Recreating this ecosystem reliably is non-trivial and high risk.
- Traceability and change control: Abruptly replacing systems that store genealogy or quality records introduces risk to continuity of evidence and to the ability to reconstruct product history.
As a result, many plants implement Industry 4.0 architecture as a series of incremental steps:
- Standardizing data collection at the edge and from existing PLCs or testers.
- Layering a data platform that mirrors and correlates data from MES, ERP, and QMS without immediately changing those systems.
- Gradually rationalizing interfaces and deprecating brittle point-to-point integrations.
- Introducing new capabilities (for example, digital work instructions or IIoT dashboards) that consume the standardized data layer.
What an Industry 4.0 architecture is not
There are several common misunderstandings:
- Not a single vendor stack: No single vendor delivers “Industry 4.0 architecture” in a box. Most plants run multi-vendor landscapes that must coexist for many years.
- Not automatically compliant: A modern architecture can support compliance, but it does not guarantee it. Validation, procedures, training, and governance are still essential.
- Not purely cloud: In many regulated or safety-critical operations, a hybrid of on-premise OT, on-premise or private-cloud data stores, and selectively used public cloud services is more realistic.
- Not a fixed blueprint: The exact architecture depends on your installed base, process criticality, regulatory requirements, network constraints, and corporate IT standards.
Constraints and dependencies
The value and feasibility of an Industry 4.0 architecture depend heavily on:
- Existing system maturity: Plants with structured MES and historian data can advance faster than those relying on paper and isolated PLCs.
- Data quality and modeling: If product, process, and equipment master data are inconsistent, analytics and automation layers will be fragile.
- Integration capability: Availability of APIs, interface documentation, and vendor cooperation significantly affects effort and risk.
- Validation and change control capacity: Regulated sites must pace changes to match the capacity of QA, validation, and operations to absorb them.
- Network and cybersecurity posture: Zoning, remote access, and patching policies can constrain which technologies and patterns are acceptable.
In practice, defining an Industry 4.0 architecture is less about drawing a perfect reference diagram and more about agreeing on a realistic target state and migration path that respects these constraints.