Using MES Analytics to Reduce Material Usage Variance in Aerospace
In aerospace manufacturing, material waste is never just a scrap problem—it is a financial event. High-cost alloys, forgings, and composite materials turn into immediate margin erosion when usage drifts beyond plan. Yet most of this waste does not come from dramatic failures. It comes from small, repeated variances that traditional systems struggle to see.
Manufacturing Execution Systems (MES) can close this visibility gap. By capturing actual material consumption, scrap, and yield at each operation, MES enables detailed analytics on material usage variance. The result is practical insight into where waste is occurring, why it is happening, and which actions will deliver the greatest financial impact.
This article explains how aerospace manufacturers can use MES analytics to track material usage variance, refine cost models, and support continuous improvement—without replacing existing ERP financial controls. For a broader view of scrap and rework, see our guide on material waste and cost visibility with MES in aerospace.
The Financial Impact of Material Waste in Aerospace
Aerospace programs are uniquely sensitive to material waste. Parts are often made from expensive, specialty materials and produced in low volumes with long cycle times. That combination makes even modest usage variance highly consequential.
High-cost alloys, forgings, and composites
Aerospace structures and engine components rely on titanium, nickel-based superalloys, advanced aluminum, and sophisticated composite systems. These materials are expensive to purchase, difficult to process, and sometimes subject to long lead times and strict qualification requirements.
Material usage variance in this context has a disproportionate cost impact:
- High raw material cost per part means that a few percentage points of over-consumption can outweigh labor savings.
- Buy-to-fly ratios for complex machined parts are already high; unplanned waste further reduces effective yield.
- Special process coupons and test samples add legitimate consumption, but lack of visibility can make them look like unexplained variance.
Effect on fixed-price and long-term contracts
Many aerospace manufacturers operate under fixed-price contracts, long-term agreements (LTAs), or rate-based pricing. When material costs rise during the life of a program, recovering those costs can be difficult or impossible.
Material usage variance directly affects:
- Program margin, especially on mature programs where price is stable but costs are still drifting.
- Make-or-buy decisions, where inaccurate internal usage data can distort comparisons to supplier pricing.
- Negotiations for future blocks or lots, where historical variance should be understood and either eliminated or built into pricing.
Without clear visibility to actual usage, finance and program management are left to explain unfavorable variances based on averages and assumptions rather than data.
Why ERP alone can’t see true usage variance
ERP systems are essential for planning, purchasing, and financial control. However, they are typically not designed to capture detailed, operation-level material usage:
- Backflush at completion only: Many ERPs backflush material when an operation or order is completed, not when material is actually consumed.
- Limited scrap categorization: ERP may record scrap quantities and value, but rarely captures enough context (operation, cause, shift) for root-cause analysis.
- Coarse granularity: ERP tends to operate at the work-order or item level, not the individual serial number, lot, or operation-step level that aerospace traceability demands.
Because of these limitations, ERP is excellent for valuing material but less effective at explaining where and why additional consumption occurs. MES fills this gap by capturing execution data as work happens.
How MES Captures Actual Material Consumption
MES connects people, machines, and materials at the point of execution. That makes it the ideal system to track real material usage and feed analytics on variance.
Issuing and backflushing material to operations
In a MES-enabled aerospace environment, material is typically associated with work as it moves through the routing:
- Material issue at operation start: Operators scan barcodes or RFID tags to issue kits, panels, forgings, or raw stock to a specific operation.
- Backflushing on consumption: For repetitive or predictable usage, MES can backflush material based on actual production quantities at that step, rather than only at order completion.
- Partial usage: The system can record partial consumption of a panel, bar, or sheet and track the remaining remnant for reuse.
This approach links specific material lots and quantities to operations and work centers, enabling much finer-grained variance analysis.
Tracking scrap and yield at each step
MES records what happens to material as parts move through the process:
- Scrap events logged with reason codes (e.g., machining oversize, layup defect, cure failure).
- Rework and repair recorded with additional material usage where allowed by engineering.
- Yield calculation at each operation, not just at final inspection.
The combination of issued material, good output, rework, and scrap enables MES to calculate actual yield by operation and by part, highlighting where material is being lost.
Serial, lot, and heat-level traceability
Aerospace programs often require traceability down to heat, lot, or individual serial numbers. MES supports this by:
- Associating each part serial with the specific material lots and heats used in its manufacture.
- Tracking consumables and process materials (e.g., adhesives, prepregs, fasteners) where they materially affect cost or quality.
- Linking inspection results and process parameters to both part and material identifiers.
This level of traceability not only supports regulatory and customer requirements, it also provides the dataset needed to analyze material usage variance across programs, lots, and suppliers.
Reporting Actual vs Planned Usage by Part and Operation
Once MES is reliably capturing material consumption and scrap, the next step is to compare it to the planned picture in your BOMs and routings.
Comparing to standard routings and BOMs
The core of material usage variance analysis is a comparison between:
- Planned usage: Quantities defined in ERP or PLM bills of material, including scrap factors and allowances.
- Actual usage: Quantities consumed and scrapped as recorded by MES at each operation.
To enable this comparison, MES and ERP must share common item numbers, units of measure, and revision identifiers. With that alignment in place, MES analytics can produce reports such as:
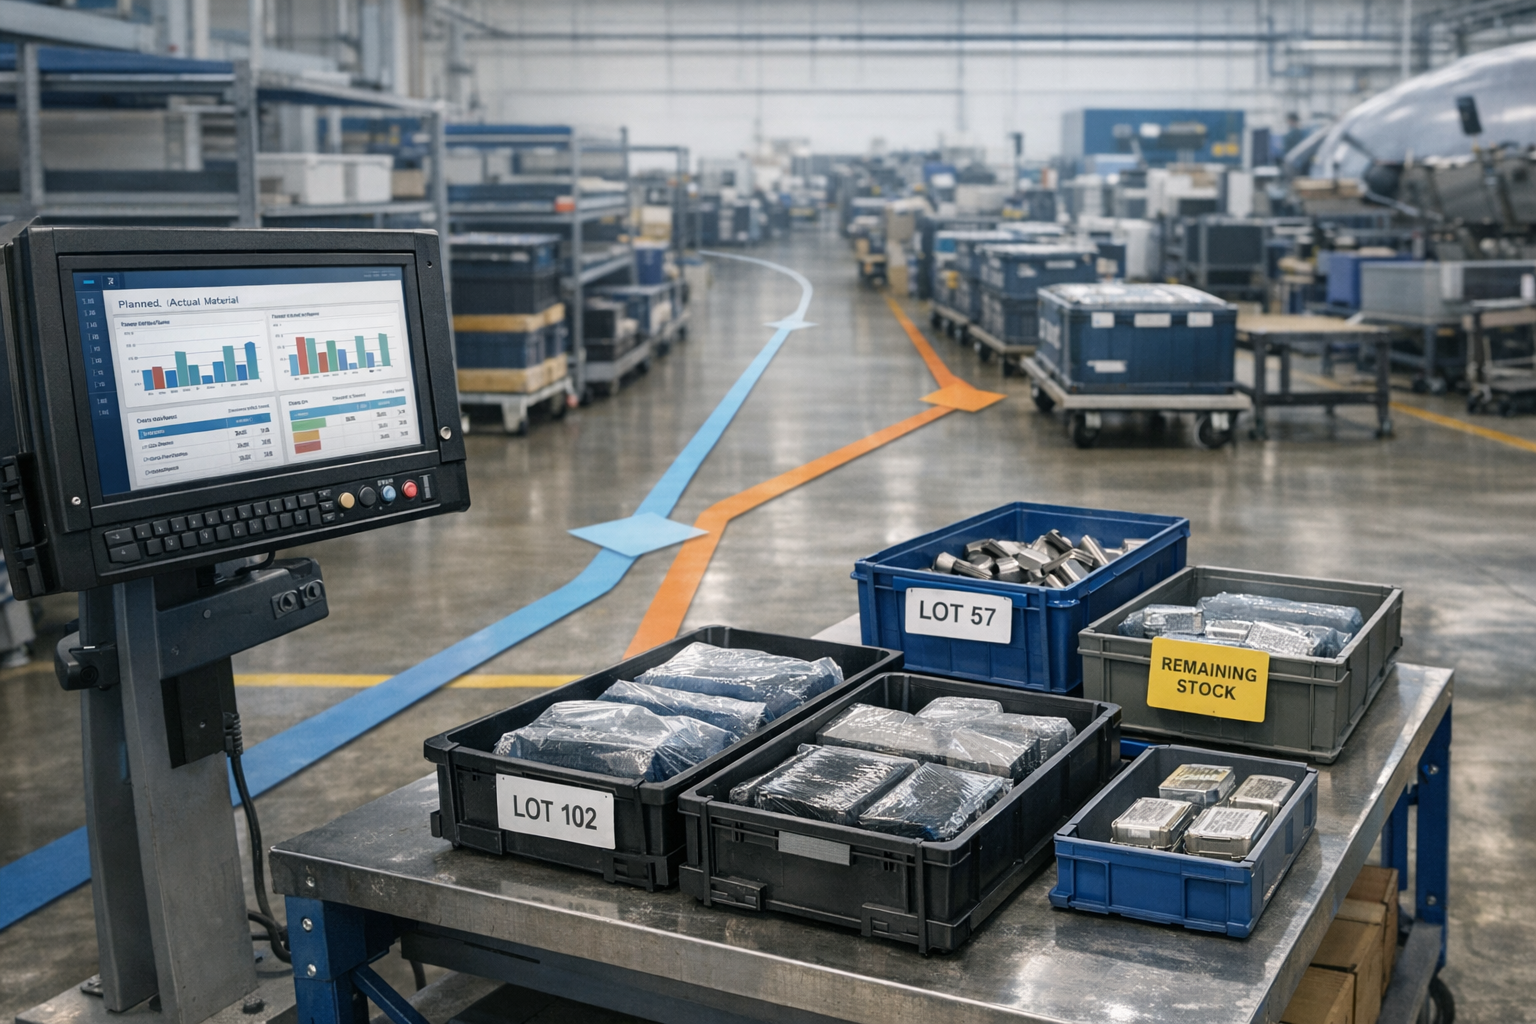
- Planned vs. actual material per part number and revision.
- Variance per operation (e.g., rough machining vs. final machining vs. assembly).
- Usage variance for specific materials across multiple part numbers.
Identifying chronic over-consumption
Not all variance is random. MES analytics can reveal chronic patterns of over-consumption, for example:
- Certain work centers consistently consuming more composite material per panel.
- Specific fixtures or tools associated with higher trim or machining scrap.
- Programs where legacy allowances significantly underestimate actual material needs.
By filtering data over weeks or months, you can distinguish between isolated incidents and systemic issues that warrant engineering or process changes.
Understanding process-driven vs random variation
MES data helps separate process-driven variance from genuine randomness by correlating usage with:
- Operation and work center: Is variance localized to a step or spread across the route?
- Shift and crew: Do certain shifts use more material due to experience levels or local workarounds?
- Material batch or supplier: Does material source affect trim requirements, yield, or defect rates?
Clarify the operational risk
When the work behind Using MES Analytics to Reduce affects quality, delivery, or compliance, teams need one place to connect evidence, decisions, and shop-floor follow-through.
Patterns in this data indicate whether you should focus on process controls, training, supplier management, or BOM assumptions.
Analyzing Scrap Drivers with MES Data
Material usage variance often originates in scrap and rework. MES provides the depth of data needed to understand these drivers and prioritize corrective actions.
Correlating scrap with work center, shift, and supplier
Because MES ties scrap to specific operations, people, and materials, you can build analyses such as:
- Scrap cost by work center, highlighting the most expensive points of failure.
- Scrap rate by shift or crew, identifying training or staffing gaps.
- Scrap by material lot or supplier, exposing quality or stability issues in the supply base.
These insights go beyond simple scrap percentages, providing a basis for targeted improvement projects and supplier discussions.
Spotting patterns in rework-driven material loss
Rework often appears to save parts, but it can quietly increase material consumption through additional cutting, patching, or component replacement. MES can show:
- How often rework leads to additional material usage (e.g., extra plies, shims, or hardware).
- Which rework paths have the highest cost per saved part.
- Operations where rework frequently fails, ultimately resulting in scrap.
With this view, engineering and operations can determine when it is better to invest in first-pass yield improvements rather than relying on rework.
Differentiating unavoidable trim from avoidable scrap
Some material loss is inherent in aerospace manufacturing. Examples include:
- Trim allowances for composite layups.
- Starter stock for machining complex shapes.
- Mandatory test coupons and process validation pieces.
MES data helps differentiate this unavoidable trim from avoidable scrap by quantifying each type and mapping it to process steps. Over time, you can refine BOM scrap factors to reflect realistic, stable levels of unavoidable loss while targeting the remainder for reduction.
Using Insights to Improve Processes and Cost Models
Collecting data is only half the job. The real value of MES analytics is realized when insights drive concrete changes in processes and financial models.
Refining allowances and scrap factors
Legacy BOMs often contain conservative scrap factors or outdated assumptions. Using MES data, you can:
- Update scrap factors by part family and operation based on recent, stable performance.
- Right-size material allowances (e.g., panel size, bar length, ply count) to better match actual needs.
- Separate regulatory-mandated scrap (e.g., coupons) from process-driven waste.
This alignment improves standard costing, quoting accuracy, and program financial forecasts.
Prioritizing continuous improvement projects
Not every variance justifies an improvement project. MES analytics support rational prioritization by showing:
- Scrap cost per operation and per work center.
- Material usage variance per part number, ranked by annual spend.
- Trend lines that distinguish worsening performance from stable, predictable variance.
With this information, engineering and operations teams can focus limited resources on the few processes that drive most of the excess material cost.
Collaborating with finance and program management
Material usage variance is as much a financial topic as an engineering one. Effective MES usage supports collaboration by providing:
- Common reports that tie together engineering scrap causes and financial impact.
- Scenario analysis for “what if” questions (e.g., what happens to program margin if we improve yield by 2% at a specific operation?).
- Evidence for price negotiations when unavoidable material costs differ significantly from original assumptions.
Importantly, MES should be positioned as complementary to ERP—providing the operational detail needed to understand and influence the financial results that ERP records.
Practical Dashboard and KPI Examples
To turn MES data into action, aerospace manufacturers typically deploy focused dashboards and KPIs around material usage and scrap.
Material yield by part family
A useful starting view is material yield by part family or product line. A dashboard might show:
- Planned vs. actual material per completed unit.
- Yield trends by month or production lot.
- Highlighting of families with the largest negative variance.
This keeps attention on groups of parts where improvements will have significant aggregate impact.
Scrap cost by process step
Another powerful view is scrap cost by process step, not just by scrap quantity. This should include:
- Material cost of scrapped parts and assemblies.
- Additional material consumed in rework operations.
- Drill-down capabilities from total cost to specific part numbers and work centers.
By ranking process steps by scrap cost, organizations can quickly identify “hot spots” worth investigation.
Top offenders by work center or program
MES dashboards aimed at leaders often include “top offenders” lists, such as:
- Work centers with the highest material usage variance this quarter.
- Programs where actual usage significantly exceeds quoted assumptions.
- Part numbers responsible for most of the variance in a given work cell.
Connect decisions to execution
Connect981 helps turn this kind of operational detail into traceable action, so the context behind each decision does not get lost.
These views promote accountability and support structured problem-solving, rather than relying on anecdotes or isolated incidents.
Governance and Data Quality Considerations
The value of MES analytics depends on data quality. Governance practices are essential to ensure the numbers can be trusted and used for decisions.
Ensuring operators record scrap accurately
Operator engagement is critical. To achieve reliable data without slowing production:
- Design simple, quick scrap entry screens with clear reason codes.
- Use mandatory fields only where they drive tangible value (e.g., operation, reason, quantity, disposition).
- Provide feedback loops by sharing reports that show how the data is used to improve processes, not just monitor performance.
Training should emphasize that accurate reporting protects programs and jobs by preventing unpleasant financial surprises later.
Aligning MES and ERP material definitions
For variance analytics to make sense, MES and ERP must speak the same language. Key alignment points include:
- Item numbers and revisions used consistently in both systems.
- Units of measure (e.g., kg vs. lb, sheet vs. m2) aligned or converted transparently.
- Material groups and cost buckets mapped so MES reports can roll up to financial categories.
Data integration should be designed so that planners and engineers do not need to maintain parallel structures in multiple systems.
Handling rework, re-melt, and recovery flows
Aerospace manufacturing often includes specialized material flows such as rework, re-melt, and recovery of scrap material. MES configurations should clarify:
- When rework consumes additional material versus simply adding labor.
- How recovered material (e.g., re-melted ingots, reclaimed test pieces) is credited back into inventory and reflected in variance calculations.
- Which scrap streams are truly lost and should be fully burdened with material cost.
Clear rules ensure that variance reporting fairly represents both waste and legitimate recovery activities.
Bringing It All Together
Reducing material usage variance in aerospace is a continuous effort, not a one-time project. MES analytics provide the factual foundation for that effort by:
- Capturing actual material usage, scrap, and yield at each operation.
- Comparing real performance to planned BOMs and routings.
- Highlighting where waste is concentrated and where process improvements will protect margins.
When combined with disciplined governance and close collaboration between operations, engineering, and finance, MES becomes a powerful enabler of margin protection and competitive pricing in demanding aerospace programs.
To see how material variance fits into the broader picture of scrap and rework reduction, explore our hub article on reducing scrap, rework, and material waste in aerospace manufacturing with MES.
For teams putting this topic into daily operation, work orders and digital travelers, shop floor execution control, a connected execution platform help connect the concept to traceability, work-order reality, and audit-ready evidence.
This article is for aerospace operations, quality, and compliance teams who need to understand Using MES Analytics to Reduce Material Usage Variance in Aerospace. It explains the practical question this topic answers in a manufacturing execution context.
The same operating model also depends on Connect981’s aerospace execution solutions, real aerospace execution examples, Connect981’s aerospace operations guidance, practical aerospace operations FAQs, especially when decisions have to move across quality, production, suppliers, and program leadership without losing context.
Frequently asked questions
An execution layer reduces risk during safety-critical engineering changes by tightly controlling how, when, and by whom new configurations are executed on the shop floor. It does not remove the need for robust engineering, quality, and configuration control, but it can significantly reduce the operational and human-factor risks associated with putting changes into production.
1. Enforcing the correct revision at the point of use
In safety-critical environments, the primary operational risk is often using the wrong revision of a design, routing, or instruction set. An execution layer can:
In practice, this connects to work orders and digital travelers when teams need to turn the answer into repeatable execution habits.
- Bind work orders, lots, and serial numbers to specific, approved engineering change revisions.
- Prevent release of work if the referenced BOM, routing, or work instruction is obsolete or not yet effective.
- Apply effective dates and configuration rules so the right version is used for each unit or batch.
- Surface only the current, approved digital work instructions to the operator, reducing reliance on tribal knowledge or printed copies.
The effectiveness of this depends on accurate and timely data from PLM, ERP, and QMS, and on validated interfaces that keep revision status synchronized.
2. Controlling who can execute safety-critical steps
Safety-critical changes often come with new skills, tools, or certifications. An execution layer supports:
- Role and competency-based access control for specific operations and steps.
- Enforcement that only qualified operators, inspectors, or special process staff can execute or sign off high-risk steps.
- Electronic signoffs with user identity, timestamp, and revision context captured for each critical operation.
This reduces the risk of unqualified personnel executing changed processes, but it requires a maintained skills matrix and integration with HR or training records, plus periodic audit of role mappings.
3. Driving correct sequencing and interlocks
Many failures around engineering changes occur when steps are performed out of sequence or prerequisites are skipped. An execution layer can:
- Enforce process flow so operators cannot move to downstream steps until required checks or measurements are completed.
- Add interlocks tied to new safety-critical steps, such as torque verification, leak tests, or functional checks introduced by the change.
- Conditionally branch workflows based on configuration, serial, or test results, avoiding manual interpretation of complex change bulletins.
This reduces reliance on memory and informal workarounds but depends on accurate modeling of routes and decision logic and on careful change control when flows are updated.
4. Embedding validation, checks, and data capture
When engineering changes alter fit, function, or safety margins, data collection and verification must follow the updated requirements. An execution layer can:
- Require capture of new parameters, measurement ranges, and evidence (e.g., photos, tool IDs, gage IDs) aligned with the change.
- Validate entries against specification limits in real time, preventing continuation if values are out of tolerance for the new design.
- Ensure calibration and tool control rules are followed when new tools or fixtures are introduced.
This helps avoid silent deviations but is only as strong as the underlying specification data, gage management processes, and the validation of the execution logic itself.
5. Managing deviations, concessions, and controlled experiments
Safety-critical changes often start with limited pilots, controlled builds, or conditional approvals. An execution layer supports structured risk handling by:
- Routing specific orders or serials through special pilot flows with additional inspections or tests.
- Linking temporary deviations, waivers, or concessions to affected work orders, and enforcing associated conditions.
- Capturing nonconformances in context if the new design or process behaves unexpectedly, with traceability back to the underlying change.
This reduces the risk of uncontrolled experiments on production hardware, but it requires disciplined configuration of special routes and clear sunset rules for temporary flows.
6. Providing full traceability of what was built, how, and under which change
When failures occur in the field, or during qualification, the ability to reconstruct exactly which revision and process were used is critical. An execution layer improves traceability by:
- Linking each unit or batch to the specific engineering change, work instructions, tooling, and parameters used during manufacture.
- Recording operator identities, signoffs, measurement data, and test results tied to the effective revision at that time.
- Maintaining an auditable history of when a change went live, where it was applied, and when it was superseded.
This does not automatically deliver compliance, but it provides the evidence needed for robust root cause analysis and formal investigations when something goes wrong.
7. Coordinating across brownfield systems
In most regulated plants, the execution layer must coexist with existing PLM, ERP, QMS, and sometimes legacy MES, along with paper-based work instructions. Risk reduction depends on:
- Reliable integration with PLM for controlled release of engineering changes and status updates.
- Clear ownership of the “source of truth” for parts, BOMs, routings, and instructions, avoiding conflicting versions across systems.
- Well-defined cutover procedures so old and new revisions are not run in parallel without proper segregation.
Attempting full system replacement during major engineering changes often increases risk because of validation burden, downtime, and integration complexity. A more practical approach is layering execution control on top of existing systems, then migrating specific functions over time under strict change control.
8. Supporting staged rollout and rollback of changes
Engineering changes can fail or have unintended side effects. An execution layer can reduce associated risk by:
- Allowing staged rollout by line, cell, program, or facility, instead of a big-bang cutover.
- Tracking adoption progress and issues in near real time through exception and nonconformance data.
- Supporting controlled rollback plans when a change must be paused or reversed, with clear rules about which units are affected and how to handle them.
This capability still relies on well-defined engineering and quality governance for go/no-go decisions and for managing partial builds or rework.
9. Capturing operator feedback and surfacing weak signals
Even well-modeled engineering changes can introduce subtle risks that only appear in execution. An execution layer can:
- Provide structured channels for operators to flag unclear instructions, unsafe conditions, or unexpected behavior related to the new process.
- Aggregate these signals with NCRs and near-miss data to help engineering and quality teams refine the change.
- Feed into continuous improvement and formal risk assessments without relying on informal communication paths.
This does not replace formal hazard analyses, FMEA, or safety cases, but it improves practical feedback loops around implementation.
10. Constraints and what an execution layer cannot do
Even with a strong execution layer, several risk areas remain outside its direct control:
- It cannot guarantee the correctness of the engineering change itself; design and analysis quality remain separate responsibilities.
- It does not, by itself, ensure regulatory or certification outcomes. Evidence and behavior must still meet external expectations.
- It must be qualified and validated like any other system used in regulated, safety-critical environments.
- If integrations with PLM or QMS are weak, out-of-date, or manually maintained, the execution layer can enforce the wrong information efficiently.
In practice, the risk reduction comes from combining a validated execution layer with disciplined configuration management, change control, training, and continuous monitoring.
There is no universal safety stock reduction number
In aerospace environments, there is no reliable “typical” percentage of safety stock reduction that automatically follows from better MES data. Reported improvements in industry case studies often quote double-digit reductions, but those numbers are highly context-specific and usually relate to a subset of materials, not the entire portfolio. The practical range you might see on *selected, well-behaved items* is often in the 5–30% band, but some items will not move at all, and a few may even need higher buffers once data reveals the true variability. Any claim of a specific percentage without looking at your demand patterns, supplier performance, and configuration complexity is essentially a guess.
Better MES data mainly improves the *confidence* and *timeliness* of information on actual consumption, yields, and constraints. That can support more accurate planning parameters, but it does not change physics, supplier lead times, or regulatory obligations. As a result, MES data can enable safety stock optimization, but it does not by itself “deliver” a fixed reduction. The actual outcome depends on whether your planning processes, ERP/MRP logic, and governance are capable of using this improved data in a controlled way.
In practice, this connects to MES execution control when teams need to turn the answer into repeatable execution habits.
Where better MES data actually helps safety stock
MES can reduce safety stock *opportunity* in several specific ways, assuming configuration and integrations are robust. First, it can tighten the feedback loop on actual consumption and scrap by serial/lot number, enabling more realistic usage variability assumptions instead of broad-brush planning factors. Second, it can provide near real-time visibility on WIP location, cycle times, and yields, which reduces the “unknowns” planners often buffer for with extra inventory. Third, it can surface machine, tooling, and process capability metrics that expose chronic variability, allowing targeted process improvements instead of compensating with stock.
MES can also support more reliable genealogy and configuration tracking, which can reduce the proliferation of slightly different part numbers or soft configurations that each carry their own small safety stock. When routing and BoM deviations, rework paths, and substitutions are captured consistently, planners can consolidate some of the fragmented inventory strategies. However, these benefits only materialize if the master data (BoMs, routings, item masters) and the MES–ERP integration are disciplined and validated. Poor integration or inconsistent usage can easily add noise, forcing planners to increase safety stock instead of decreasing it.
Constraints specific to aerospace and regulated environments
Aerospace programs often cannot reduce safety stock as aggressively as less-regulated industries due to certification, configuration control, and lifecycle support requirements. Safety stock is not just a buffer for lead-time and variability; for many items, it is also an insurance against obsolescence, supplier exit, or qualification lead-time that can run to many months or years. For certified parts and materials, adding or changing suppliers carries a heavy qualification and documentation burden, so planners may choose higher stock levels even if MES reveals stable consumption.
Configuration complexity and long product lifecycles also limit reductions. Multiple variants of the same platform, block upgrades, and long-term spares obligations create small, slow-moving demand streams that do not lend themselves to lean buffers. In some fleets, regulatory or contractually committed service levels effectively set a lower bound on safety stock, regardless of MES visibility. Better MES data can eliminate *unnecessary* buffers caused by poor visibility, but it cannot override these structural constraints.
Why outcomes vary so much between plants and programs
Safety stock outcomes differ widely even within the same company, largely due to differences in process maturity and system coexistence. Plants with relatively clean item masters, stable routings, and disciplined use of MES transactions can often trust the data enough to revise planning parameters. In contrast, brownfield sites with multiple legacy MES instances, partial integrations, and workarounds (e.g., offline travelers, spreadsheet planning) may not see usable data improvements quickly, even after a new MES rollout.
Program context also matters. A mature program with stable design, established suppliers, and predictable demand is better positioned to reduce buffers once MES data confirms stability. A new or frequently changing program, or one facing recurring configuration changes and field retrofits, may decide to maintain higher buffers despite improved data because underlying variability remains high. The same MES capabilities can thus support material reductions in one context and merely confirm that existing buffers are appropriate in another.
Dependence on ERP/MRP, planning rules, and governance
Even perfect MES data does not reduce safety stock unless the planning layer (usually ERP/MRP or APS) is instrumented to use that data. Safety stock levels are typically driven by parameters such as target service level, forecast error, lead-time variability, and lot-sizing rules. If these parameters are never revised, or if planners override system suggestions based on local heuristics, improved MES data will have limited impact. In some cases, exposing more variability through MES actually leads planners to *increase* buffers to maintain service levels.
To translate better MES data into reduced safety stock, companies need: validated MES–ERP integrations, clear ownership of planning parameters, and controlled processes for updating those parameters based on measured variability. Change control and documentation are especially important in aerospace, where any systematic parameter changes can affect downstream commitments and may be scrutinized during customer or regulatory audits. Without this governance, attempts to “optimize” safety stock based on new MES data can introduce new risks instead of removing old ones.
Practical ranges and how to think about targets
In practice, many aerospace organizations that deliberately use MES data in a structured inventory optimization effort see modest but meaningful improvements. A realistic pattern is: some materials (typically C-class or stable consumables) might show 10–30% reductions, some A/B items might allow 5–15% reductions, and a non-trivial fraction will remain unchanged. On certain programs, the net effect may be a single-digit percentage reduction in total inventory value, but concentrated in specific families where risk is manageable. In other cases, the reward is primarily *avoided increases* in safety stock as complexity grows.
Rather than chasing a universal percentage, it is more robust to treat MES-enabled safety stock optimization as an ongoing, item-class and program-specific exercise. Set targets by material segment and risk profile, not by a global percentage. Track where reductions are justified by data and where constraints such as qualification, contractual service levels, or single-source dependencies prevent change. This keeps expectations realistic and avoids forcing reductions in areas where they would create unacceptable supply or compliance risk.
Scope and purpose: what each system is trying to solve
MES and ERP track material usage for different primary reasons, even when they hold overlapping data. ERP is usually oriented around planning, inventory valuation, procurement, and financial reporting, so its material usage focus is on quantities, locations, and costs at a part-number and lot level. MES is oriented around executing work on the shop floor, so material usage is tracked at the level of specific units, serials, and work steps tied to orders or build records. In aerospace, this means ERP answers questions like “how much of this alloy do we have and what does it cost?” while MES answers “exactly which heat/lot/serial went into this specific assembly and which operation performed the installation?”.
Granularity and genealogy requirements in aerospace
For aerospace and defense, MES is typically the system that can track full material genealogy down to individual serials and process steps. This includes which operator performed the work, which resource or cell was used, what version of the work instructions were followed, and which certifications or inspections were associated. ERP usually cannot maintain this level of granularity without custom extensions or add-ons, and even then is rarely used as the source of truth for unit-level genealogy. In practice, the MES production record often becomes the primary traceability record, with ERP referencing it indirectly through order, lot, or serial numbers. When material traceability is audited, the expectation is usually that MES (with supporting systems like PLM/QMS) can reconstruct the detailed as-built/as-maintained structure rather than ERP alone.
In practice, this connects to materials planning and erp integration when teams need to turn the answer into repeatable execution habits.
Data model: how material usage is represented
In MES, material usage is commonly modeled as consumptions tied to specific operations, work centers, and production orders, often down to serial-number, batch, or kit identifiers. The data model usually supports many-to-one relationships such as multiple component serials per assembly serial, as well as partial consumption and scrap recorded in real time on the shop floor. ERP typically represents material usage through inventory movements (issues, returns, transfers) at a storage location or warehouse level, with optional lot or batch attributes and costing elements. While some ERPs can store serial-level detail, they generally do not capture the full process context (operation, machine, environmental conditions, signatures) that aerospace programs rely on. Aligning these different models without gaps or conflicts requires deliberate master data design and disciplined usage patterns across both systems.
Real-time execution versus planning and reconciliation
MES is used during execution to ensure the right material is consumed at the right step, enforcing constraints such as material status, expiry, required inspections, and approved substitutions. It can block execution if the wrong lot or serial is scanned or if calibration/qualification conditions are not met, which is critical in aerospace builds where misapplied material can have safety and airworthiness implications. ERP typically sees material usage as part of inventory and financial movements that can tolerate short delays and later reconciliation. That means discrepancies between what MES thinks was consumed and what ERP shows as issued can occur if integration or procedures are weak. Maintaining alignment requires clearly defined integration patterns where MES events drive ERP postings (or vice versa) and robust exception handling for missed or failed transactions.
Traceability, audits, and regulatory expectations
In aerospace programs, auditors and customers typically expect end-to-end traceability from finished assemblies back to raw material lots, including the ability to show when and where a particular material was installed and under which conditions. MES is generally better positioned to provide this because it connects material usage with process data, operator actions, and quality checks in a single record. ERP can show that specific lots were purchased, received, and issued, but without the manufacturing context it often cannot answer critical questions about specific builds or deviations. However, auditors may still pull ERP data for stock status, lot histories, and financial controls, so both systems must be consistent. Any gaps between MES records and ERP inventory can become findings, so reconciliation processes and periodic checks are as important as the system capabilities themselves.
Integration, validation, and common failure modes
The main technical risk is assuming that material tracking in MES and ERP will stay aligned automatically without rigorous integration design and validation. Common failures include delayed or missing postings from MES to ERP, partial updates that do not handle scrap or rework correctly, and mismatched master data (e.g., units of measure, lot IDs, or substitution rules). In regulated aerospace environments, fixing these issues is not just an IT exercise; changes to integration logic, data models, or workflows often trigger impact assessments, regression testing, and re-validation. Plants also face downtime and training constraints that limit how aggressively they can rework legacy integrations. As a result, many sites operate with known gaps and compensate with manual reconciliation and local controls, which may be acceptable only if the residual risk is explicitly understood and managed.
Replacement versus coexistence in brownfield aerospace environments
MES does not replace ERP for material usage in aerospace; it complements and extends it. ERP remains the backbone for purchasing, inventory valuation, and financial reporting, while MES is the execution system providing detailed as-built records and enforcing material-related constraints on the floor. Attempts to push all traceability into ERP or to discard ERP in favor of MES usually run into qualification and validation burdens, complex re-integration with surrounding systems, and unacceptable downtime risks. Aircraft and ground test assets have long service lives, so traceability records must remain coherent for decades, making large-scale data migrations particularly risky. Most aerospace manufacturers therefore operate both systems in parallel, with clear boundaries of responsibility and disciplined interfaces, rather than betting on a single system to do everything.
Connecting this to practical aerospace material tracking
If your specific concern is ensuring reliable material traceability on a program or site, focus first on clarifying which system is the system of record for unit-level genealogy (usually MES) and which is the system of record for inventory and financials (usually ERP). Then, define exactly how events flow between them: when MES consumption triggers ERP issues, how rework and scrap are posted, and how you detect and correct mismatches. Be explicit about where approvals, signatures, and controlled records live so that audit trails are defensible. Finally, treat integration changes as controlled changes subject to impact analysis and validation, rather than quick IT fixes, because subtle errors in material usage synchronization can propagate silently for years and only surface during an incident or deep audit.